
Motionwell designs and builds cleanroom automation equipment: machines that have to run inside a classified room without spoiling its particle class. The cleanroom automated test equipment carries 4 to 6 fan filter units in its own ceiling and holds ISO Class 7/8 over the test fixtures. Our tray-fed filling and sealing machine for a medical and pharmaceutical customer was designed to sit inside an ISO Class 7/8 room, on a stainless frame with a stainless product-contact path whose grade and surface finish follow the cleaning chemistry. This page is about the machine: what changes in the frame, the drives, the cables, the lubricant and the enclosure when the equipment has to hold a particle class while it is moving.
That last part is where cleanroom machine design gets interesting. A machine is a particle source that you are about to place inside the one space you spent money keeping clean. It has bearings that wear, belts that shed, cylinders that exhaust, cables that flex, and an operator who opens it. Every one of those is a design decision made months before anyone runs a particle count.
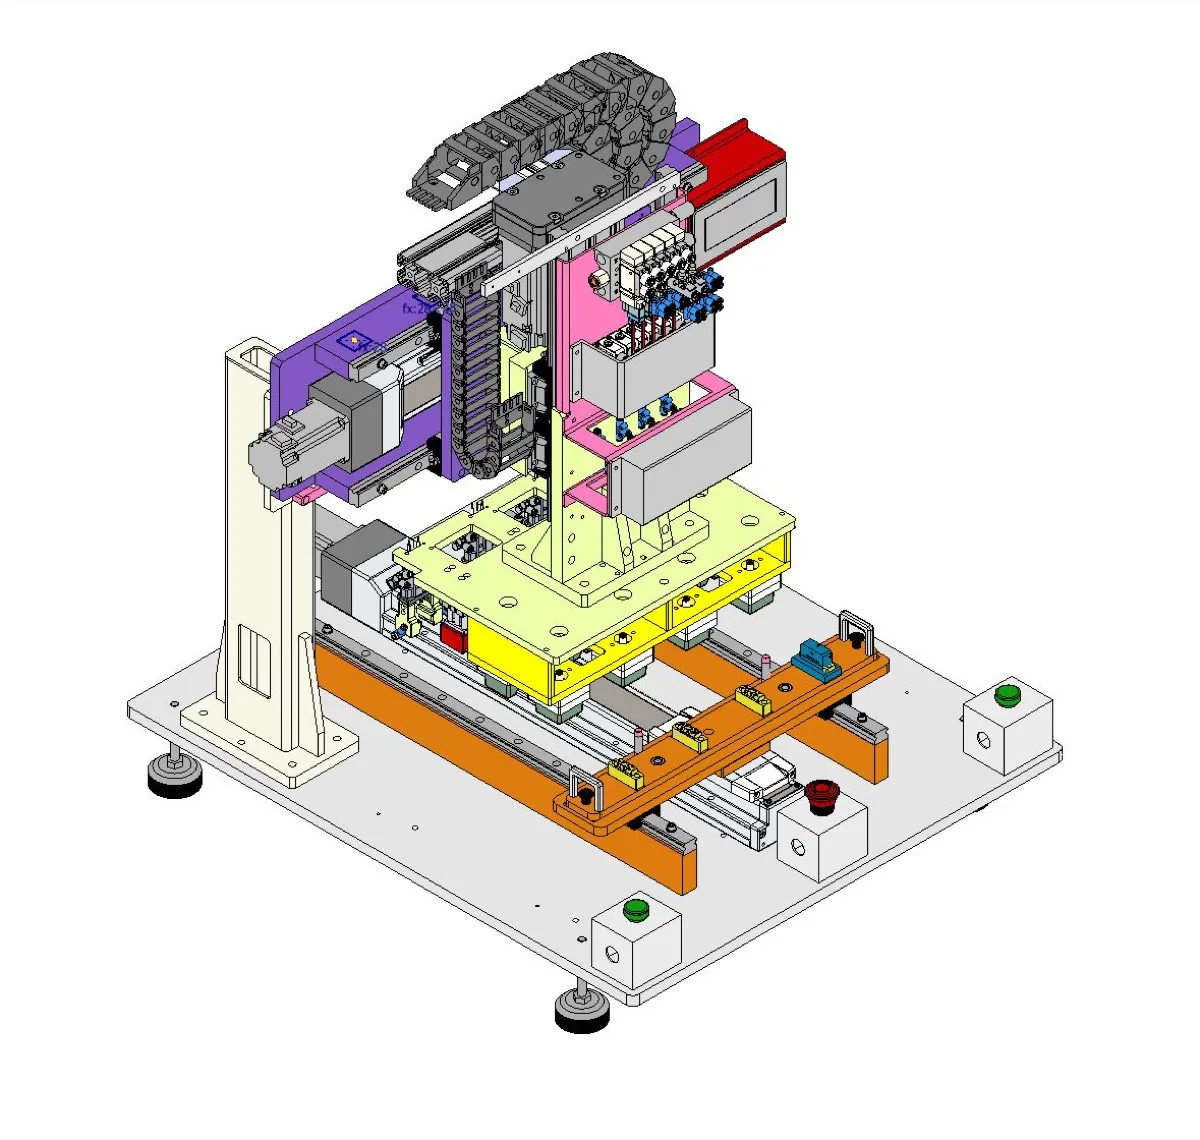
What Makes a Machine Cleanroom-compatible?
Four properties have to hold at once, and they pull against each other.
The machine must not generate particles, which is the constraint that reshapes the mechanism, because anything that slides, rolls, meshes or flexes wears and that wear becomes airborne. It must not outgas either: plasticisers, uncured adhesive, standard grease and some cable jackets release volatiles that condense on product surfaces, and nothing looks dirty while yields drop.
It has to survive cleaning, which means every external surface takes a wipe of isopropanol or a quaternary disinfectant several times a shift for years, and blind holes, exposed bolt heads and lap joints are the places a wipe cannot reach. And it must not wreck the airflow, because a machine standing under unidirectional downflow is an obstruction: flat tops create recirculation, and deep external recesses hold what the airflow was supposed to sweep away.
For scale, ISO 14644-1 allows 352,000 particles at 0.5 um and larger per cubic metre at Class 7, and ten times that at Class 8. A factor of ten between two adjacent classes sounds generous until you realise the machine itself has to fit inside that budget alongside the operators, the product and the facility. Getting the mechanism right early is the cheapest lever you have, which is the same argument that runs through our approach to custom special purpose machine design generally.
How Does Cleanroom Class Change the Machine Design?
The target particle class sets the environment the machine must support. Material, finish and enclosure choices follow the process, cleaning chemistry, exposed product and particle sources. Use the class together with these inputs to write the equipment specification.
| Design aspect | Selection input | Design and verification task |
|---|---|---|
| Frame | Cleaning agents, corrosion exposure and proximity to product | Select a compatible metal and finish; make joints accessible for cleaning |
| External finish | Residue limits and cleaning method | Specify surface roughness, crevice control and polishing where they support the cleaning process |
| Cable routing | Flexing, wear and airflow around the product | Enclose particle-generating carriers and seal entries into the clean zone |
| Pneumatics | Exhaust location and air quality | Filter or route exhaust away from the protected process; verify during cycling |
| Motors and drives | Heat, wear and maintenance access | Position drives and exposed mechanisms outside the protected zone where practical |
| Lubrication | Volatility, particle release and material compatibility | Select the lubricant and containment for the duty and service interval |
| Documentation | Room classification state and process qualification | Record the operating configuration, sampling plan, cleaning procedure and acceptance results |
Two entries in that table cost the most money. Moving the servo drives outside the enclosure means a longer, shielded motor cable and a separate control cabinet, which changes the footprint. Ducting pneumatic exhaust out of the clean zone means every cylinder gets return tubing back to a manifold instead of a muffler on the port, which changes the pneumatic schematic and the cable carrier fill.
Do not over-specify. If the product only needs Class 8, buying Class 5 sealing buys you a machine that is harder to maintain for no yield benefit.
Which Materials, Coatings and Surface Finishes Belong in a Cleanroom Machine?
Metals. Anodised aluminium (6061-T6, hard anodise on wear surfaces) and stainless steel carry the structure. Bare aluminium sheds oxide. Mild steel corrodes under the cleaning chemistry and then sheds rust, so it does not belong anywhere a wipe reaches. Where product touches metal, it is stainless.
Polymers. PEEK, POM, UHMWPE and PTFE behave. Nylon is hygroscopic and swells, and standard rubber outgasses and sheds. Static seals are typically Viton or EPDM, chosen against the cleaning agent fluid, because the disinfectant is what attacks them daily.
Coatings and adhesives. Powder coat is fine on a Class 8 enclosure and a liability above it, because chipped coating is a particle source that grows over the machine’s life. Anodise the aluminium, passivate or electropolish the stainless, and keep adhesives low-outgassing and fully cured before the machine ships.
Geometry. Cleanability is drawn in. No blind holes. Generous internal radii, with no sharp internal corners. Countersunk or counterbored fasteners. Welded seams ground flush, with no lap joints forming a crevice. Unused threaded holes plugged.
How do we decide the product-contact surface finish?
On our tray-fed filling and sealing machine for a medical and pharmaceutical customer, the product-contact path is stainless steel and the machine was designed to run inside an ISO Class 7/8 room. The roughness figure on a wetted path like that is a specification we settle with the customer, not a house standard we carry over: it follows the cleaning and swabbing regime the process is validated against, and the residue limit that regime has to reach. Electropolish, a mechanical polish and a mill finish answer different residue limits at different cost, so the target belongs in the URS next to the cleaning validation. Surfaces that never touch product, on that machine or on the cleanroom test equipment, only have to survive the disinfectant wipe-down, so the wipeable, crevice-free standard in the table above is what they are held to, and a polished roughness figure buys nothing there.
The general rule is that the finish follows how the surface gets cleaned and how much residue is allowed to survive that cleaning.
Where Do the Particles Actually Come From?
Cleanroom particle generation inside a machine has three main sources, and all three are decided on a drawing long before anyone runs a counter: the mechanism that moves, the air that leaves the machine, and the boundary between the two.
Guides, screws and belts
Linear guides, ball screws, timing belts and gear trains generate particles by design. In a normal factory nobody cares. Inside a classified zone the options are: enclose the mechanism in a sealed housing with local extraction, move it below the product plane so downflow carries debris away from the part, or select a low-particle variant with sealed wipers and cleanroom grease. Bellows over a ballscrew are cheap. Reworking a gantry after the first particle count is not.
Pneumatic exhaust
A standard cylinder with a muffler on the exhaust port vents oil-laden air into the room on every stroke, at the exact moment and location the tooling is over the product. This is usually the single largest particle source on a machine and the easiest to miss on a drawing, because the schematic looks identical either way. The fix is a cleanroom-rated cylinder with its exhaust ported back to a manifold outside the clean zone. Catch it at schematic stage and it is a line on a drawing. Catch it on the first particle count and it is every actuator on the machine re-plumbed, with the tooling already built around the port positions the old cylinders had.
Motors, drives and the enclosure boundary
Motor cooling fans move unfiltered air. Servo drives have their own fans and heatsinks. The usual answer is a boundary: particle-generating hardware on one side, product on the other, with panels gasketed continuously and fasteners captured so a screw cannot drop into the process. Where an axis must cross that boundary, it crosses through a sealed bellows or a glanded penetration.
Vision hardware needs the same treatment. Cameras and their lighting run warm, and many carry their own cooling airflow, which puts a heat source and an air mover directly over the product, so on cleanroom builds they belong behind a sealed window. The optical trade-offs of doing that are covered in our machine vision inspection guide.
How Should Cables, Drag Chains and Lubricants Be Chosen?
Cabling in a cleanroom machine is a contamination question before it is a tidiness question.
- Jacket material chosen for low outgassing and low particle shedding; PTFE and FEP for the tightest classes, PVC acceptable in Class 7/8 builds.
- Individually glanded cable entries. One large cutout backfilled with silicone is not a seal, it is a future leak path.
- Continuous-flex cable inside energy chains rated for the travel. Ordinary installation cable in a moving chain works for a while and then crazes at the jacket, and a crazed jacket inside a chain is a particle source no wipe-down reaches, because the debris is made where nobody can see it and shaken out over the product.
- Stainless cable ties in place of nylon, which sheds as it is tensioned and again as it ages.
- Bend radius respected. A jacket cracked at a tight bend becomes a particle source that no wipe-down will fix.
- Permanent laser-etched or engraved labels. Paper labels and printed tape shed fibre.
Lubricants matter for the same reason and get overlooked more often. Standard machine grease outgasses and can migrate to product surfaces. PFPE greases sold for cleanroom and vacuum service are the usual substitute, applied to sealed bearings in small quantities. Over-lubrication is a contamination source in its own right, so the maintenance instruction has to specify a quantity and an interval, not “grease as required”.
When Is a Fan Filter Unit Better than a Cleanroom?
A fan filter unit wins when only the process needs classified air and the rest of the building does not.
Fan filter units mount in the machine’s own ceiling, push HEPA-filtered air down over the process area, and let it exit through filtered vents at the base. The clean zone travels with the machine. You are buying filters, a gasketed ceiling panel and pressure monitoring instead of building construction, facility HVAC capacity, gowning airlocks and the recurring cost of maintaining a classified room around equipment that only needs a clean envelope over one fixture.
The design work is in the airflow. The FFUs have to move enough air downward to sweep particles off the product before the machine’s own motion stirs them back up, and the internal layout has to leave that downflow a clear path. Tall fixtures, overhead tooling and a poorly placed cable tray all create a shadow where the flow does not reach. Positive pressure inside the enclosure has to be maintained relative to the factory, or the room leaks into the machine every time the door seal moves.
It is not the right answer everywhere. If your product needs classified air along its whole route, well past one station, you need the room.
How the fan filter units are integrated into the test equipment
The cleanroom automated test equipment for electronics and semiconductor customers carries 4 to 6 fan filter units sealed into the enclosure ceiling with continuous gaskets, holding ISO Class 7/8 over the test fixtures and the part handling area while the machine sits in a normal factory bay with no classified facility around it.
Getting that to hold in production needs a few things designed in from the start: an unobstructed downward path over the fixtures, filtered return at the enclosure base, differential pressure monitoring so anyone can see the enclosure is still positive, and sampling ports so a particle counter can verify the class without dismantling anything. The build is described further in the cleanroom ATE case study.
How Does Wipe-down Change the Enclosure Design?
Wipe-down is a daily mechanical event that the machine has to survive thousands of times, and it drives more geometry than most specifications admit.
Every external surface has to be reachable in one pass with a wiper, which rules out deep recesses, ledges and exposed fastener heads. Cleaning chemistry attacks seals and labels, so gaskets are selected against the disinfectant and labels are etched. And because a wipe-down cannot reach inside the enclosure, maintenance access has to be planned: put service points on the non-clean side wherever the mechanism allows, and where an access panel must open into the clean zone, it gets a documented re-clean and re-qualification step. Every maintenance event that breaks the boundary is a contamination event unless someone wrote the recovery procedure down.
The same thinking applies to guarding. Interlocked doors, light curtains and access panels are safety hardware assessed under ISO 13849-1:2023 and contamination boundaries at once, which is why the guarding layout and the airflow layout have to be resolved together. Our approach to that is set out under machine safety and compliance.
How Do You Prove the Machine Holds Its Class in Production?
At-rest and operational measurements answer different questions. Test the required operational state with the axes moving, pneumatic devices cycling and operators performing the specified tasks. That measurement shows how equipment and people affect the protected process during production.
That is why particle count verification belongs in performance qualification. The counter samples at defined points around the process area during a real production run, and the result either shows the mechanism stays inside the particle budget under motion or it shows which axis does not. For regulated customers this sits inside the wider IQ/OQ/PQ package, which we cover in detail under computer system validation and equipment qualification.
The design consequence is simple: settle the sampling points and the acceptance criteria at concept stage, because they decide where the access ports go and how the enclosure is divided.
Which Cleanroom Machine Types Does Motionwell Build and Design For?
Electronics test with on-board clean air comes first. Automated test equipment with 4 to 6 fan filter units integrated into the machine ceiling holds ISO Class 7/8 over the test fixtures without a classified facility around it.
On a multi-station rotary indexing assembly machine for medical disposables, the cleanroom compromise is at its sharpest: high-rate indexing motion and an enclosed, wipeable structure have to share the same footprint. The indexer, the station drives and their pneumatic exhaust would sit below a sealed dial plate, ducted out of the clean zone, so that only the tooling and the product are above the boundary and the in-line vision stations look through sealed windows. How we lay that out is set out in how we design multi-station rotary assembly machines, and the wider context sits on our medical device automation page.
Filling and sealing for medical and pharmaceutical work runs on a tray-fed machine with a three-head dosing station, a stainless frame, a stainless product-contact path and an enclosure designed for an ISO Class 7/8 room. What it doses, how tightly and how fast are decided by the liquid, the container and the seal method, so those numbers are quoted against your products and never inherited from an earlier build. Dosing is done with diaphragm dispense valves, which keep the actuator out of the fluid path, so the only wetted moving part is a diaphragm that is changed as a consumable without opening the rest of the product path inside a classified room. The build is written up in the filling and sealing machine case study, and related work on pharmaceutical packaging lines covers the downstream side.
Laboratory and QA environments make up the fourth group. Repeat work across the QA lab transformation programme put mobile robots, a collaborative robot and vision into a controlled laboratory space, where the constraints on transport, cabling and surface finish overlap heavily with cleanroom builds. That work is described under automation for laboratory and QA environments.
Which Five Mistakes Show Up on the First Particle Count?
Designing the machine, then making it cleanroom-compatible. Cleanroom requirements sit in the frame, the fasteners, the cable route, the motor choice and the pneumatic schematic. All of those are early decisions. Revisiting them late means redoing the frame and rewiring the machine, which is most of a rebuild.
Treating wear debris as a maintenance problem. Guides and belts shed because that is what they do. Either enclose them, drop them below the product plane, or specify low-particle variants. No cleaning schedule compensates for a mechanism that sheds into the product path.
Leaving pneumatic exhaust on the cylinder. This one recurs across projects, because it is invisible on the schematic and obvious on the particle counter.
Building a flat-topped, recessed enclosure. Under unidirectional flow, a flat top creates recirculation and external recesses trap what the airflow should carry away. Slope the top and keep the outside geometry simple.
Assuming maintenance is somebody else’s problem. If a bearing change requires opening the enclosure inside the clean zone and nobody wrote the re-clean procedure, the machine goes out of qualification the first time it is serviced.
What Do We Need from You to Specify a Cleanroom Machine?
To get a useful design proposal, we need three things from you:
- The particle class the product actually requires, and where it is required. Over the whole process, or only at one station? That single answer decides between a facility cleanroom and machine-integrated fan filter units.
- The cleaning regime: what chemistry, how often, and by whom. It sets the surface finish, the seal material and the label type more directly than the ISO class does.
- The qualification scope, whether that is GMP, ISO 13485 or a customer protocol, and whether particle counting under motion is part of acceptance. It changes the documentation effort and the sampling port layout.
Send those along with your cycle time and part description through our contact page and we will come back with a design approach, including a straight answer on whether you need a classified room at all.