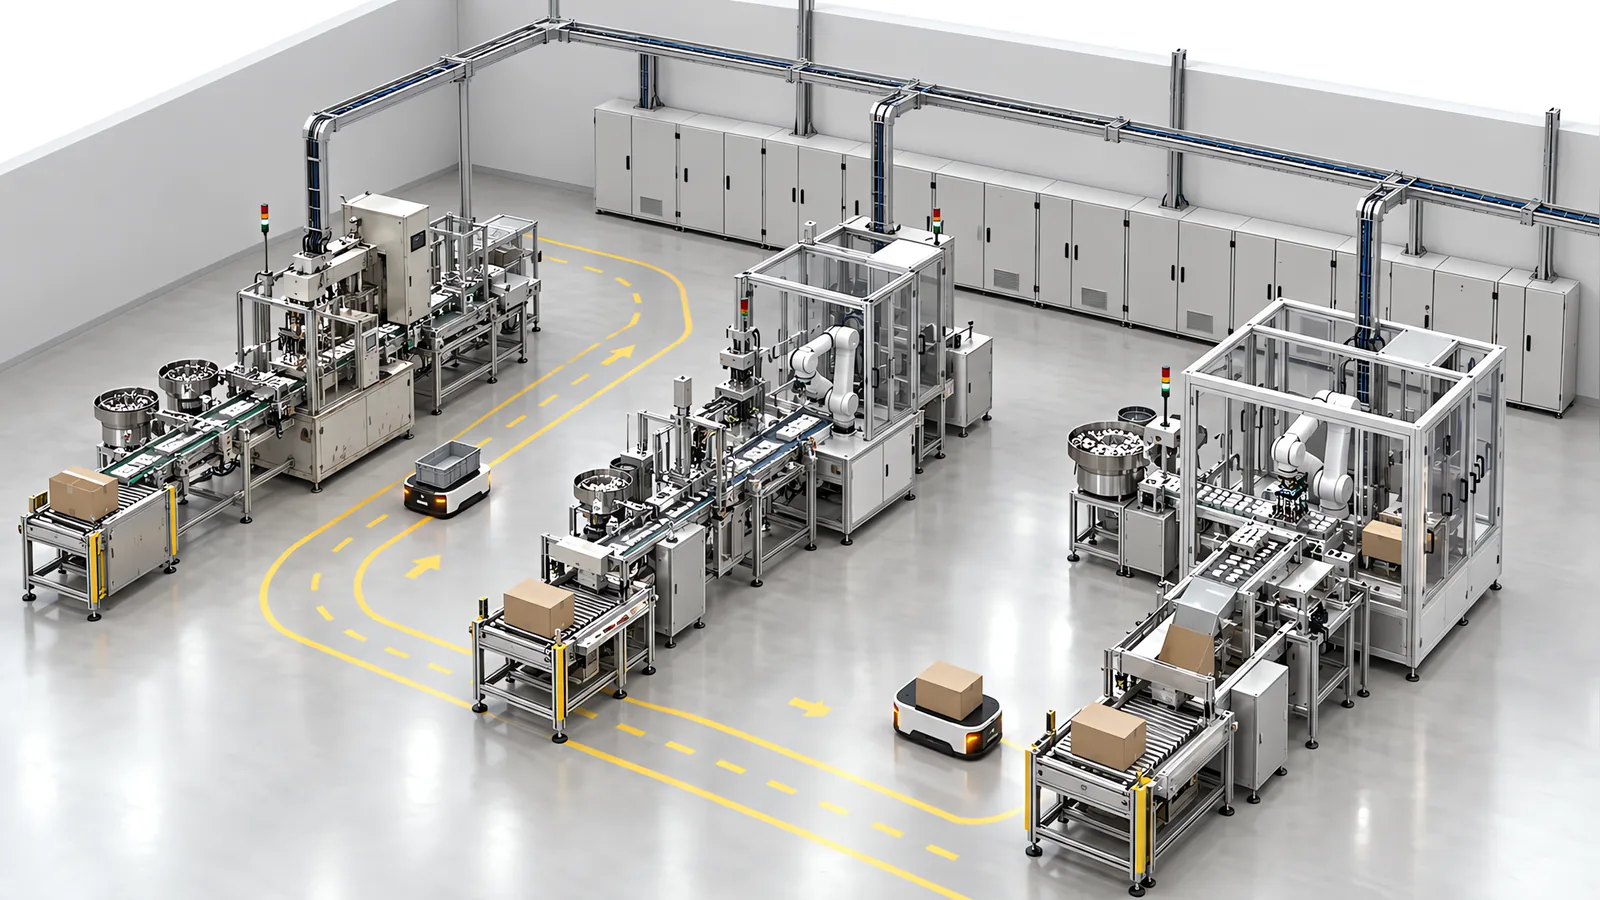
Turnkey factory automation coordinates several production lines, connections to existing equipment and shared control standards as one programme. Alongside the machine designs, it needs a phase order and a plan for four shared resources: shutdown windows, maintenance and controls staff, staging space, and building utilities.
Motionwell has designed, built and tested automation in Singapore since 2014. Factory work can combine new assembly and packaging equipment with intralogistics, legacy-machine connections and control-system replacement. Planning those packages together helps each phase fit the plant that is already operating around it.
What a turnkey contract transfers on one line, and where the supplier boundary falls, is set out on our turnkey automation systems page, and the phase-by-phase delivery model is explained in what turnkey automation includes. This page is the level above both: ordering the phases, attaching them to equipment you already own, deciding how far to standardise the control layer, and cutting the programme into packages.
What Does Turnkey Factory Automation Cover That a Single Line Does Not?
Four decisions need a programme owner coordinating the individual projects.
The order of the phases. Each line can be justified on its own numbers and still be the wrong one to build first, for reasons set out in the next section.
The shared procurement content. Compare the controller, drive and other component families proposed across phases. Where duties and maintenance needs align, coordinated orders can simplify sourcing and spare holdings. Check delivery dates and design maturity before combining purchases, so a later phase’s changing requirements do not delay equipment already needed on site.
The interfaces between phases that do not exist yet. Line two will hand product to a line three nobody has designed. Why the later purchase carries the accommodation is worked through in what turnkey automation includes. The factory level adds a timing point. Written on paper before phase one is quoted, the convention is a paragraph in an enquiry. Settled after phase one is running, it is a modification to a machine in production, priced as one.
The capacity of the building. Review power, air, extraction and floor loading across all planned phases. Coordinate connected loads, simultaneous demand and available capacity with facilities engineering, then include any upgrades in the programme schedule.
| What the factory level owns | What happens when no one owns it |
|---|---|
| Phase order | The line with the most available budget goes first, and the line that is the constraint waits |
| Common long-lead items | The same drive family is ordered three times, on three lead times, at three prices |
| Conventions for interfaces not yet designed | Nothing is written down, so every later package has to be surveyed for the convention before it can be quoted |
| Utility headroom across all phases | The last phase discovers the switchboard, the compressor or the floor loading is the limit |
| Your own engineers’ time | Two commissioning programmes land in the same fortnight and neither gets the people |
| One standard for documentation and tags | Four lines, four tag conventions, and no way to compare them |
Which Line Should Be Automated First, and What Decides the Order?
Review six factors together. The priority depends on the intended benefit and on practical constraints such as product maturity, shutdown access and available engineering staff.
What benefit is the phase meant to deliver? For a throughput project, measure the plant’s constraint and the losses that reduce its output. A non-bottleneck task can still justify automation through quality, safer handling or reduced manual work; evaluate those benefits directly. Our OEE measurement guide explains the production data needed for the throughput case.
Is the product frozen? A design freeze is what a machine gets built against. Where the product on a line is still moving, that line belongs later in the programme and earlier in the concept work, so the engineering is ready when the drawing stops changing.
Can the line be handed over in pieces? Whether a process can be broken at a buffer is settled on our turnkey automation systems page. At programme level that answer sorts the candidates against the calendar. Lines that can be cut fit the short windows that come round several times a year. Lines that cannot must wait for the one long shutdown, and if two are in the plan they compete for the same week before anybody has drawn a layout.
Does the window exist in the calendar? Record the available hours on specific dates, including isolation, installation, tests and production restart. Match the phase scope to that window before committing its site milestone.
Will the learning transfer? Use the first phase to test proposed controller conventions, tag names, alarm structure, documentation and acceptance templates. A representative line makes the results easier to reuse. If the first line has unusual requirements, separate its exceptions from the common plant standard.
Does it share long-lead content with later phases? Where two phases want the same drive family or the same safety components, running them close together buys one order and one set of spares. Where they share nothing, separating them in time frees your engineers, which is the resource that actually runs out.
| Candidate first phase | Argument for going first | What it costs to go first |
|---|---|---|
| The measured constraint | Additional usable capacity can increase plant output once the process is commissioned | Production access and ramp-up need careful planning at the current bottleneck |
| A line with a natural buffer | It fits a short window, and it is a cheap place to learn | The benefit arrives in instalments |
| A representative line with a stable product | Conventions written here are reusable across the plant | The return may be smaller than another line’s on paper |
| The line with the easiest approval | The money is available now | If its process is unrepresentative, separate its exceptions before using it as the plant template |
| A line already due for a control upgrade | The machine is open anyway, so the tie-in costs once | Scope has to be settled early enough to catch the retrofit window |
The last row can reduce repeat disruption. A control upgrade may already require cabinet access, wiring changes and recommissioning, creating an opportunity to add the planned interface. Confirm the signals, software and shared tests early enough to include them in that shutdown; the existing panel may be retained or replaced according to the upgrade scope.
How Do Turn-Key Automation Systems Attach to Equipment You Already Own?
Start with a survey of the physical transfer and the available control signals. Check part position, transfer height, buffers, cycle capability and the states the existing controller can expose to the new line.
A plant-level programme reaches existing equipment, and each of those machines was specified by whoever needed it at the time, against that year’s budget and whichever supplier’s house platform it came with. What it leaves is a control estate with several controller families, panel brands and programming environments in one building, which is the normal starting condition and not a sign of neglect. Count it before the programme starts, one row per machine: controller family, panel, drive family, network, and whether anybody on site can open the program. It is a short list to make and it is what the plant standard has to be written against.
Three tie-in shapes cover nearly everything, and the ladder between them, including what each can and cannot tell you, is on our legacy machine connectivity page. What belongs at the factory level is the choice of shape per machine, and that choice is commercial before it is technical.
The question to ask about each existing machine is not which interface is best. It is when that machine is next going to be opened. A machine whose controller is out of support, or whose safety circuits are due, is going to be touched inside the programme window anyway, and the tie-in should ride along with that work. A machine that is sound and supported deserves the least invasive interface that carries the signal, which is frequently a dry contact and a counter. The routes out of a control upgrade, including the cases where the right answer is a new machine, are argued on our machine retrofit and modernisation page, and the platform side is on our PLC migration page.
Keep an integration register for each phase: the machines included, interface changes, risk-assessment owner and required conformity records. For EU-market equipment, review modifications against the European Commission’s machinery scope guidance. Link the resulting decisions and validation evidence to the machine and drawing revisions in the register.
How Far Should the Control Layer Be Standardised Across the Plant?
Far enough that the lines can be read and maintained together, and no further, because every mandate you add has to be enforced on every bid. A plant wide control standard earns its keep on the maintenance side, so write it as the short list of things a night shift needs to be the same everywhere and leave the rest to whoever builds each line.
Prioritize conventions that affect maintenance across lines: supported control platforms, consistent tag names, comparable stop reasons and recoverable software archives. Keep application-specific mechanical choices with the machine design, while documenting any parts the plant needs to standardize for service or spares.
Four things are worth mandating in a purchase specification.
The controller family for new builds. Your technicians are the reason. A platform your maintenance team stocks, programs and has been trained on is worth more than a marginally better controller nobody on site can open at two in the morning. Mandate it, and run a written waiver route for the cases where a motion requirement genuinely does not fit.
The tag and device naming convention. Issue it with the enquiry so drawings, software and data interfaces use the same names from the start. Retrofitting a convention requires review of affected programs, screens, reports and tests.
The alarm-to-stop-reason mapping. An alarm list that does not map to a downtime reason produces four lines whose stop data cannot be added up. How alarms and screens should be organised inside a machine is on our HMI and SCADA integration page; what belongs in the plant standard is the mapping.
The network and address plan. The plant retains ownership and approval of the network policy. Its IT/OT team can develop the detailed design with the integrator, then control the allocation of addresses, access routes and changes across phases.
Keep working HMIs on tie-in machines where they remain supportable and expose the required functions. Component-family standards can also help with spares and training, but apply them selectively. Review exceptions where force, motion, environment or availability calls for a different component.
| Standard | Worth mandating? | What enforcing it costs | What happens without it |
|---|---|---|---|
| Controller family for new builds | Yes, with a waiver route | Some price competition, and occasional platform mismatch on hard motion | Maintenance carries four programming environments and four sets of spares |
| Tag and device naming | Yes, with documented legacy mappings | Design and interface review time | Data needs additional mapping before it can be compared |
| Alarm to stop-reason mapping | Yes | A list your team has to write once | Downtime data that cannot be added across lines |
| Network and address plan | Yes, owned by the plant | Design, review and change control with a named owner | New connections may bypass intended segmentation or create address conflicts |
| Electrical build standard | Yes, stated per destination market | Include its design and verification work in the quotation | Panels may be built to different expectations |
| HMI brand on tie-in machines | No | Replacing working panels to satisfy a rule | A mixed panel estate, which is the normal condition anyway |
| Component families for service and spares | Selectively, with an exception route | Compatibility review and possible sourcing constraints | More spare variants and training needs where commonality would have been practical |
The electrical build row has a standard behind it. IEC 60204-1 governs the electrical equipment of machines, covering supply disconnection, protection against shock, stop categories, conductor identification and documentation, and it is the counterpart to NFPA 79 for a machine built for the United States market. The destination market therefore has to be settled before panel design starts on any phase, and in a multi-site group that answer can differ per line. How a panel scope is actually drawn, and what a plant keeps on its own side of it, is covered in what an electrical system integrator's scope covers.
What Does Connecting Every Line Do to the Factory Network?
Connecting lines creates communication paths between production equipment and plant systems. Those paths need a planned security boundary, approved traffic and controlled service access.
A brownfield expansion may reuse existing switches and network infrastructure. Check that the added ports preserve the intended zones, VLANs, access controls and communication routes. Reusing a switch can be practical; connecting a new line without updating the segmentation design can expose traffic beyond its intended boundary.
Prepare an address and segmentation plan before phase one, with capacity for the later phases. Following the risk-based approach in ISA/IEC 62443, group assets into zones with compatible security requirements and define the permitted communication conduits. A production line may contain several zones. The plant approves the policy and change process; the integrator can design, implement and test the agreed controls. Our IEC 62443 guide explains the roles and engineering steps.
Specify the clock source and time-synchronisation method in the network plan. Comparable timestamps help trace a stop through several machines and correlate production events with server records.
When Should a Factory Programme Be Split Across Several Vendors?
Define packages around measurable acceptance outcomes and explicit interfaces. A package may have several metrics, such as rate, quality and mission completion. Keep a named owner for the end-to-end result where the metrics depend on equipment from several suppliers.
Three cuts are usually right.
Along technology families with clear handover points. Intralogistics and assembly need different trials. A mobile robot fleet can be tested on mission throughput, delivery time, charging and traffic at defined pickup and drop-off points, then tested with the production lines it serves. Compare a specialist package with a lead-integrator scope based on who will coordinate those interfaces. ASRS versus AGV covers the material-flow selection.
Along windows. Separate shutdowns can use independent phase packages, or staged releases under one master contract. Compare design maturity, interface ownership, procurement commitments and acceptance dates. Keep each phase’s site window and dependencies visible under either structure.
Where keeping a second builder alive is worth paying for. Price discovery and continuity are legitimate reasons to award phase two elsewhere. The cost is that you own the standard and the interface list between packages, which is work.
Review splits inside a line carefully. Separate mechanical and controls packages need a lead responsible for the combined rate and shared tests. Tie-in work needs a common survey and interface specification with the affected machine supplier. Price and schedule that coordination explicitly.
| Cut the programme along | Good reason | Poor reason |
|---|---|---|
| Technology family | Intralogistics, assembly and packaging need different engineering and different acceptance | The lines merely look different on a layout |
| Shutdown window | Each package is accepted inside the window it owns | Phases are in different budget years but the same window |
| Plant or site | Different buildings, different occupiers, different duties | Head office prefers one purchase order |
| Second source on purpose | Price discovery and continuity, with the standard held by you | Awarding on price alone, then asking the winner to match conventions they never saw |
| Inside one line’s rate | Specialist scopes with a named integration lead and shared line test | Separate hardware and controls awards with no owner for the combined result |
Use the turnkey automation systems scope to review each phase’s new equipment, existing-machine interfaces and acceptance needs. The mix can change as earlier phases enter production. Packaging line integration explains balancing equipment from several makers; turnkey assembly automation covers the single-line purchase and commissioning plan.
What Should You Ask Vendors of Turnkey Automated Production Lines?
Use these seven questions to review a bidder’s relevant experience and proposed delivery plan. Look for project records and clear responsibilities, not just an equipment list.
- Show a line where you tied into a machine you did not build. Who wrote the handshake, and what was available on the old machine? The answer tells you whether brownfield work is experience or aspiration.
- On comparable lines, who owned the tag convention, you or the plant? Ask how the bidder maps existing equipment and implements a customer’s convention.
- What is in the handover pack, by document name? Schematics, I/O list, program archive, alarm list with stop reasons, spares list, maintenance procedures. Ask to see a redacted example.
- Will you quote phase two against our standard, and which exceptions do you propose? Review the engineering reason, cost and maintenance implications of each exception.
- Who is on our floor for the first production week, and for how long? The first week is a project stage whether anybody scheduled it or not.
- What lifecycle and support information is available for the proposed platform? Review the manufacturer’s current notices, update policy and migration options, including where an end-of-support date has not yet been announced.
- Which items are made to drawing, bought in or single-source? Ask for the critical procurement dependencies and who obtains the required supplier records. The sourcing plan is more useful than supplier count alone.
The longer framework for scoring builders against each other, including us, is in our guide to choosing a system integrator in Singapore and in how to choose a special purpose machine builder. What belongs in the enquiry itself, before any of those questions get asked, is covered by our note on writing an automation URS.
What Gets Written Once and Reused on Every Line After It?
A short plant automation standard, owned by you, attached to every enquiry. This is the asset a multi-line programme produces, and the first phase pays for it whether or not anybody writes it down.
Five documents carry it. The tag and device naming convention. The network and address plan with the clock source named. The safety function register format, so each phase’s register can be read by the same people. The handover deliverables list with the alarm-to-stop-reason mapping included. And the acceptance protocol template, stating how a rate is counted and over what run length.
Keep the plant standard focused on repeatable operating and maintenance needs. Specifying a component family can be useful for spares interchangeability, mounting conventions or training. Include an exception route where the required force, motion, environment or availability calls for a different choice.
Two ownership points decide whether the standard survives. It needs an owner at the plant, and at this level that has to be a role with the standard written into it, not whichever engineer ran phase one, because the document has to outlive that person’s next move. And it has to be issued with the enquiry, since a convention introduced during detail engineering is a change order. What an unowned record costs on the repeat enquiry is argued in what turnkey automation includes, and the project mechanics each phase runs through are on our automation project process page.
Where Should a Factory Automation Programme Start?
Start with the intended benefit and the existing production flow. These seven planning questions help define the phases; the plant team and integrator can work through them together.
- Which line sets the plant’s output today, measured?
- Which lines have a product that is frozen, and which do not?
- Which phases have a real window, stated as hours on dates?
- Which existing machines are due to be opened anyway inside that period?
- What does the building provide in total, across every planned phase?
- Who at the plant owns the standard, and who owns each interface row?
- Who runs and maintains all of this in year two?
| Your situation | Start from | Why |
|---|---|---|
| Several lines wanted, nothing measured yet | A benefit and constraint study on the existing flow | Separate throughput gains from quality, handling and labour benefits |
| One clear bottleneck, other lines stable | A single line, with conventions written as if there will be more | The cheapest intervention that still produces a reusable standard |
| Mostly existing machines, few new builds | Tie-in and control upgrade scope, phase by phase | The value sits in interface work, so buy that directly |
| Multi-site group with differing market requirements | The plant standard first, stating the electrical and conformity position per site | The destination market changes panel design and documentation |
| A shutdown window that cannot carry a whole line | Phased scope with station-level acceptance | The window sets the package boundary, so the scope is drawn to fit the hours available |
| No internal controls team, and none planned | Fewer platforms, deeper documentation, longer support scope | The platform choice is a maintenance decision before it is a technical one |
Two rows applying at once is normal in a plant, and at this level it is a sequencing question before a contracting one. Decide which row the first phase answers, and let the second set the phase after it.